10 Best Gate Valve Manufacturers for Global Buyers
Choosing the right gate valve manufacturer can influence plant safety, operating costs, and long-term maintenance. A dependable supplier must offer more than attractive pricing. Buyers need proven engineering, consistent materials, accurate machining, and responsive technical support.
Piping authority Mohinder L. Nayyar emphasizes, “Valve selection begins with the service, not the valve name.” This principle remains practical. A gate valve for clean water faces different demands than one handling steam, abrasive slurry, or corrosive chemicals. Pressure class, temperature range, sealing design, body material, and actuation method all require careful review.
This guide examines ten respected gate valve manufacturers serving international markets. It considers manufacturing experience, product range, testing procedures, certifications, delivery capability, and after-sales support. It also looks at details buyers often miss, including casting quality, stem protection, packing access, and spare-part availability.
Small details matter.
A valve may look excellent in a catalog. Field performance can tell another story. Some suppliers provide strong documentation but limited customization. Others offer flexible production yet uneven delivery times. No ranking is perfect, and market conditions change.
The selected manufacturers represent different strengths. Some focus on large-diameter industrial valves. Others specialize in forged designs, oil and gas applications, water systems, or severe-service equipment. Global buyers should compare these strengths against their own operating conditions.
A careful decision includes more than a brand name. It includes inspection records, material traceability, realistic lead times, and clear communication. That is where reliable sourcing begins.
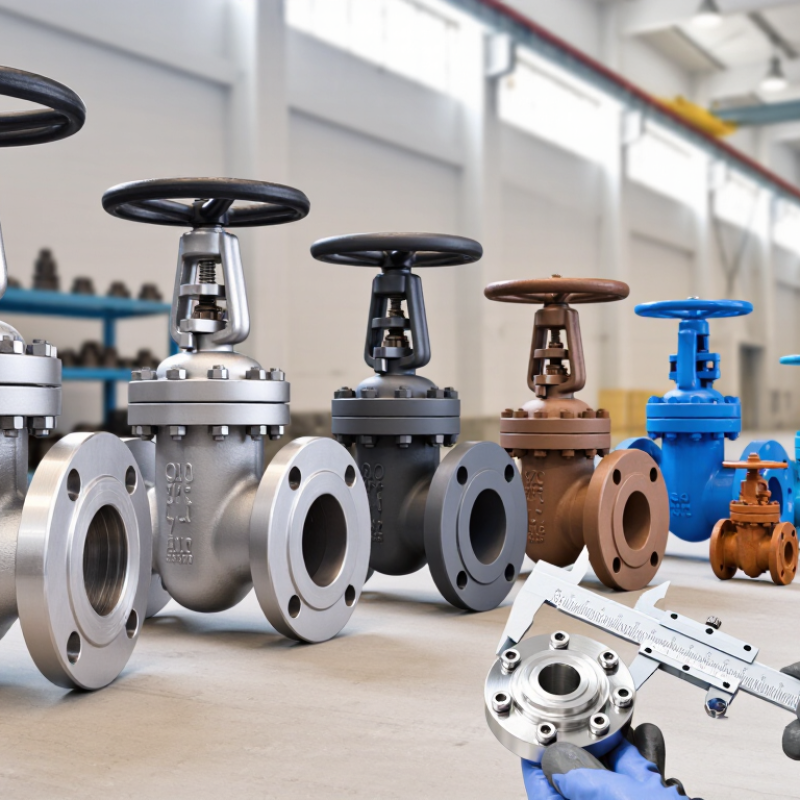
Table of Contents [Hide]
What Defines a Leading Gate Valve Manufacturer
A leading gate valve manufacturer proves performance beyond a polished catalogue. According to Fortune Business Insights, the global industrial valves market was valued at over USD 78 billion in 2023. That scale increases buyer risk. Experienced manufacturers should provide pressure-test records, heat-number traceability, and clear material certificates. Their designs should align with relevant standards, including API 600, API 6D, ASME B16.34, and ISO 15848 where applicable. Standards alone are not enough. A valve must suit the fluid, temperature, pressure, and operating frequency.
Reliable production also depends on repeatability. Buyers should examine machining tolerances, wedge alignment, seat leakage results, and coating controls. The U.S. Department of Energy has reported that industrial valves can contribute significantly to compressed-air and process losses when leakage is ignored. This makes testing more than paperwork. It becomes an operating-cost issue. A capable manufacturer also offers practical engineering support, realistic lead times, spare-part planning, and documented corrective actions. No supplier gets every detail right. The honest ones show how they fix recurring failures.
Tips: Request a sample inspection dossier before placing a large order. Check whether test data identifies the actual valve, not only the product series. Ask for field references in similar pressure classes. Confirm factory acceptance procedures early. A low purchase price may hide costly commissioning delays. Also, do not judge quality from weight alone; heavier is not automatically better.
Key Criteria for Comparing Global Gate Valve Suppliers
10 Best Gate Valve Manufacturers for Global Buyers
Key Criteria for Comparing Global Gate Valve Suppliers
Choosing among gate valve manufacturers requires more than comparing catalog prices. Global buyers should verify operating pressure, temperature, media, and pipe size first. A valve for abrasive slurry needs different trim than one for clean water. Fit matters. Ask for test records, material certificates, and drawings before placing an order. Experienced suppliers explain failure risks instead of promising universal performance.
Technical quality should be measurable. Review design standards, pressure-test procedures, coating systems, and inspection points. Confirm whether each valve receives shell and seat testing before shipment. Traceable heat numbers on body and stem materials add confidence during audits. Suppliers with documented corrective actions often deserve closer attention. Still, paperwork can look perfect. Inspect the process, not only the folder.
Compare delivery reliability, spare-part access, communication speed, and after-sales support across regions. A low purchase price may become expensive when a replacement seat waits six weeks at a port. Request a realistic production schedule, export packing details, and remote troubleshooting procedures. Evaluate total cost over the valve’s service life. No checklist is perfect. Field feedback may reveal issues that factory samples miss. Revisit supplier performance after installation, especially if torque rises, leakage appears, or handwheels corrode.
10 Best Gate Valve Manufacturers for Global Buyers - Key Criteria for Comparing Global Gate Valve Suppliers
| Supplier Profile | Typical Product Strength | Common Size Range | Typical Pressure Classes | Body and Trim Materials | Applicable Standards | End Connections | Actuation Options | Quality and Certification Indicators | Suitable Industries | Indicative Lead Time | Best Evaluation Advantage |
|---|---|---|---|---|---|---|---|---|---|---|---|
| Profile 01 | General industrial resilient-seated gate valves | DN 50–DN 600 | PN 10–PN 16; Class 150 | Ductile iron, cast iron, carbon steel; stainless steel trim | EN 1074-2, EN 1171, ISO 5752 | Flanged, wafer, lugged | Handwheel, gearbox, electric actuator | ISO 9001; pressure and shell testing; WRAS or equivalent where applicable | Water treatment, irrigation, HVAC, utilities | 4–8 weeks for standard sizes | Balanced price, availability, and standardization |
| Profile 02 | Bolted-bonnet carbon-steel gate valves for process plants | DN 50–DN 900; NPS 2–36 | Class 150–Class 600 | WCB carbon steel; 13% chromium or stainless steel trim | API 600, API 598, ASME B16.34 | ASME flanged, butt-weld, socket-weld | Handwheel, bevel gearbox, electric actuator | ISO 9001; material traceability; PMI and hydrostatic testing | Oil and gas, petrochemical, power generation | 8–14 weeks | Strong documentation and process-industry compliance |
| Profile 03 | Forged gate valves for high-pressure service | NPS 1/2–NPS 4 | Class 800–Class 2500 | Forged carbon steel, alloy steel, stainless steel | API 602, ASME B16.34, API 598 | Threaded, socket-weld, butt-weld, flanged | Handwheel or compact electric actuator | Heat-number traceability; NDE; fugitive-emission testing where specified | Refineries, chemical processing, steam systems | 10–16 weeks | Compact construction and high-pressure capability |
| Profile 04 | Stainless-steel gate valves for corrosive media | DN 15–DN 300; NPS 1/2–12 | PN 16–PN 40; Class 150–300 | CF8M, CF3M, duplex stainless steel; PTFE or metal trim | API 600, API 603, ASME B16.34 | Flanged, butt-weld, socket-weld | Handwheel, gearbox, pneumatic or electric actuator | Positive material identification; corrosion-resistant material certificates | Chemical, pharmaceutical, food processing, marine | 8–14 weeks | Material selection for aggressive or hygienic environments |
| Profile 05 | OS&Y gate valves for municipal water networks | DN 50–DN 1200 | PN 10–PN 25 | Ductile iron body; EPDM seat; stainless steel stem | EN 1074-2, EN 1171, ISO 7259 | Flanged, restrained, grooved by project specification | Handwheel, square operating nut, electric actuator | ISO 9001; potable-water approval; coating inspection | Drinking water, wastewater, water transmission | 5–10 weeks | Large-diameter supply and infrastructure compatibility |
| Profile 06 | Metal-seated gate valves for abrasive slurry service | DN 50–DN 600 | PN 10–PN 40; Class 150–300 | Ductile iron, carbon steel, stainless steel; hardened or alloy trim | EN 1074-2, API 598, MSS SP-81 where applicable | Flanged and wafer-style connections | Handwheel, gearbox, pneumatic or hydraulic actuator | Wear testing; coating verification; seat leakage testing | Mining, minerals processing, dredging, ash handling | 8–16 weeks | Wear resistance and maintainability in difficult media |
| Profile 07 | Cryogenic gate valves for low-temperature applications | NPS 1/2–24 | Class 150–Class 600 | Austenitic stainless steel; extended bonnet; low-temperature trim | BS 6364, API 602 or API 600 as applicable, API 598 | Flanged, butt-weld, socket-weld | Handwheel, gearbox, pneumatic or electric actuator | Cryogenic testing; low-temperature impact testing; helium leakage testing where specified | LNG, industrial gases, cryogenic storage | 12–20 weeks | Low-temperature sealing and specialized testing |
| Profile 08 | Bellows-sealed gate valves for zero-emission process service | DN 15–DN 300; NPS 1/2–12 | PN 16–PN 100; Class 150–600 | Carbon steel, stainless steel, alloy steel; welded metal bellows | EN 1983, API 600, ISO 15848 where specified | Flanged, butt-weld, socket-weld | Handwheel or gearbox | Fugitive-emission testing; bellows cycle testing; material traceability | Chemical, pharmaceutical, vacuum, hazardous-fluid systems | 12–18 weeks | Reduced stem-emission risk and enhanced containment |
| Profile 09 | Slab or expanding gate valves for pipeline service | NPS 2–48 | Class 300–Class 1500 | Carbon steel, low-temperature carbon steel, stainless steel trim | API 6D, API 598, ASME B16.34 | ASME flanged, butt-weld | Handwheel, gearbox, electric or hydraulic actuator | API 6D certification; fire-safe testing; fugitive-emission testing; NDE | Transmission pipelines, terminals, oil and gas infrastructure | 14–24 weeks | Pipeline isolation, piggability, and double-block capability |
| Profile 10 | Engineered-to-order gate valves for power and utility projects | DN 50–DN 1500; NPS 2–60 | PN 16–PN 420; Class 150–2500 | Carbon steel, alloy steel, stainless steel, hardfaced trim | ASME B16.34, API 600, API 602, EN 1984 | Flanged, butt-weld, pressure-seal bonnet designs | Handwheel, gearbox, electric, pneumatic or hydraulic actuator | Design verification; NDE; hydrostatic testing; project-specific inspection plans | Power generation, steam networks, district energy, utilities | 16–28 weeks | Engineering support and compliance with complex project specifications |
Note: The profiles represent common global gate-valve manufacturing capabilities. Actual size, pressure rating, materials, certifications, testing scope, pricing, and lead time should be confirmed against the supplier’s current technical documentation and project specifications.
Profiles of Ten Notable Gate Valve Manufacturers
10 Best Gate Valve Manufacturers for Global Buyers
Profiles of Ten Notable Gate Valve Manufacturers
Global gate valve demand is shaped by oil, gas, water, power, and process industries. Fortune Business Insights estimates the industrial valves market reached about USD 78.49 billion in 2023. It projects continued growth through 2032. Procurement teams now examine testing records, delivery stability, and service support, not price alone.
The ten profiles represent different manufacturing strengths. One specializes in API-certified valves for refineries. Another focuses on cryogenic service and low-temperature sealing. A third supplies large-diameter waterworks valves with epoxy-coated bodies. The fourth serves power plants with pressure-seal designs. A fifth offers compact forged valves for chemical lines. The sixth combines regional production with fast replacement parts. A seventh emphasizes automated machining and traceability. The eighth supports mining sites with abrasion-resistant components. The ninth targets municipal projects and resilient-seat designs. The tenth provides custom valves for high-pressure pipeline systems.
Details matter. A casting defect can hide beneath a smooth coating. Poor stem alignment may appear only after repeated cycling. ISO 5208 testing, API 598 inspection, and documented material certificates improve buyer confidence. The 2024 MarketsandMarkets industrial valves analysis also identifies infrastructure investment and process automation as major growth drivers. Still, published capability claims require careful checking. Factory audits, sample inspections, and reference projects remain useful. No profile is flawless. Regional approvals, spare-part access, and repair skills can change the real purchase value. A cheaper valve may create higher downtime costs later.
Gate Valve Types, Standards, and Industry Applications
Gate valves isolate flow rather than regulate it. Common designs include wedge, parallel-slide, knife, and resilient-seated types. Wedge valves suit water, steam, and process lines. Knife gates handle slurry, pulp, and dry solids. They cut through difficult media.
Standards define safer purchasing decisions. API 600 and API 602 cover steel gate valves for industrial service. ASME B16.34 addresses pressure-temperature ratings, materials, and testing. ISO 5208 and EN 12266-1 specify pressure tests and leakage acceptance. A practical review should check body material, trim, seat design, stem arrangement, and end connection. Small details matter. A rising stem needs clearance above the handwheel. A buried valve may require a non-rising stem and a longer operating key.
Demand is broad. Grand View Research valued the global industrial valves market at about USD 78.4 billion in 2023 and projected growth through 2030. Its figures combine several valve categories, so they cannot predict gate-valve demand alone. That limitation deserves attention. Buyers serving refineries often specify carbon steel, alloy trim, and fire-tested construction. Water projects usually prioritize corrosion resistance, low operating torque, and resilient seats. Mining systems need abrasion-resistant materials and accessible maintenance points. The International Energy Agency’s 2024 World Energy Investment report also shows continuing capital flows into power and grid infrastructure, where isolation valves remain essential. Local certification, inspection records, and documented test results should be verified before shipment. Specifications are often clear; installation conditions are not.
How Global Buyers Can Select the Right Manufacturer
Selecting among the 10 best gate valve manufacturers requires more than comparing online rankings. Global buyers should match each manufacturer’s experience with the project’s actual conditions. Check valve size, pressure class, temperature range, media, and installation environment. A supplier experienced with seawater service may not suit high-temperature steam applications.
Request technical drawings, material certificates, pressure-test records, and traceability documents. Verify whether the factory follows recognized standards and maintains consistent inspection procedures. An independent inspection before shipment can reveal casting defects, damaged seats, or incomplete coatings. Small details matter.
Ask for references from similar projects, not only famous customers. Review delivery performance, communication speed, spare-part access, and warranty handling. A factory audit can show whether machining equipment is modern or heavily worn. Photos are useful, but production records are stronger evidence.
Price needs careful interpretation. I once treated a low quotation as efficiency; later, extra testing and replacement costs changed the calculation. It was an expensive lesson. Compare total ownership cost, including freight, installation, maintenance, and downtime. A reliable manufacturer should explain limitations clearly, even when the answer may reduce the order. That honesty is worth more than polished sales language.
